

Depaneler setup, from crate to first clean cut
Bench, air, knife gap and stage alignment on the VPD3-1M and the VPD5-330, in the order the operation manuals run them, with every number in inches and millimeters.
A depaneler that cuts badly on day one is almost never a bad machine. It is a bench that is not level, a gauge nobody read, or a knife gap that was never set with a feeler. All of it is an hour of work, and all of it is in the book that ships in the crate. This is that hour, split into the three jobs it actually consists of.
Before you touch a knife: on the VPD5-330, close the sliding hand valve and confirm the gauge reads zero. On the VPD3-1M, engage both carriage end locks. Handle every blade by the back edge only.
-
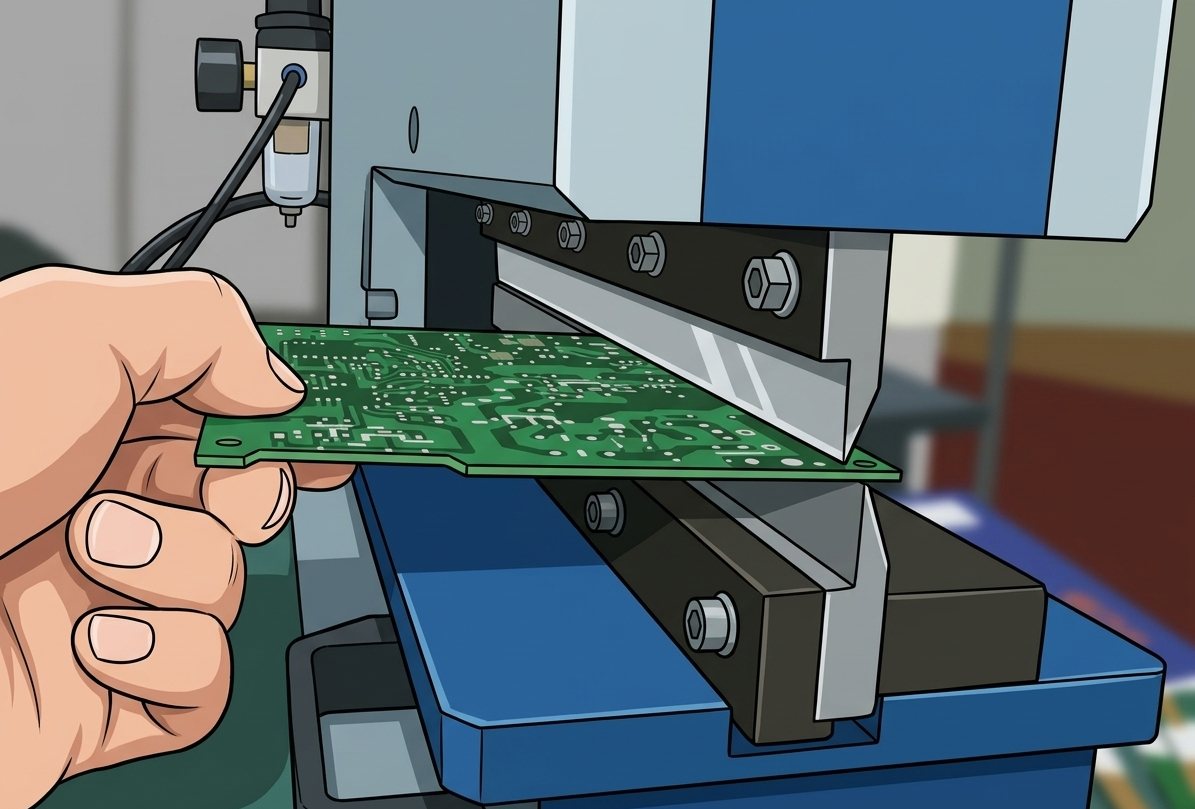 Pneumatic
VPD5-330 bench, air and first cut
Bonding the chassis, the three air fittings, what the panel gauge has to read, the foot switch, and the first panel through.
Five steps →
-
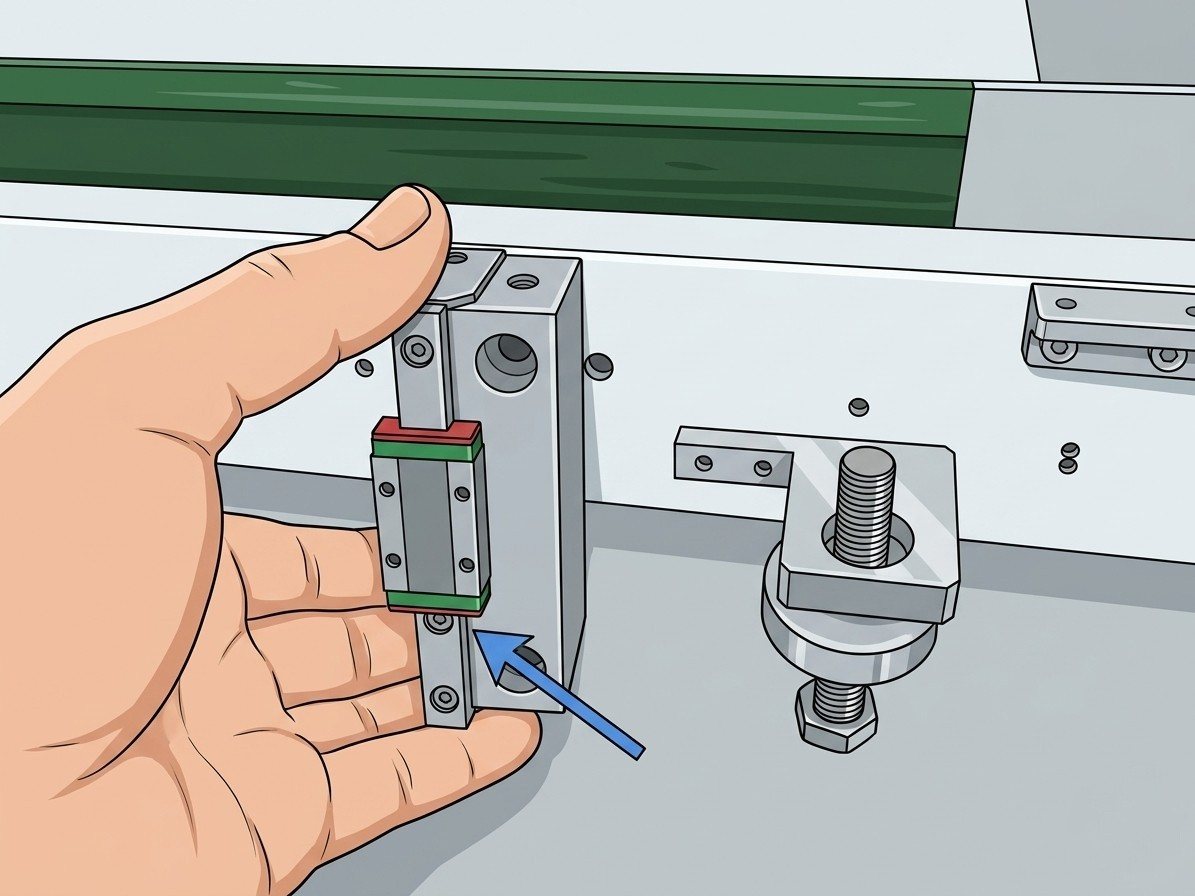 Manual
VPD3-1M stage and linear slides
The stage ships detached. Getting it onto the slides square, in the order that makes it drop on instead of fight you.
Six steps →
-
 Both machines
Blade gap and alignment
The 0.05 mm feeler, the opening gap at the knob, the jam nuts and the Blade Calibrator. Needed again after every knife change.
Read the procedure →

The numbers worth writing on the bench
| VPD3-1M | VPD5-330 | |
|---|---|---|
| Cut length | 290 mm (11.42 in) | 330 mm (12.99 in) |
| Unit weight | 35 kg (77 lb) | 125 kg (275 lb) |
| Bench | Rated 60 kg (133 lb) or better | Stable, level, ESD safe with a verified ground bus |
| Air | None. Hand operated | 6 bar (85 psi) at the panel gauge, dry and oil free |
| Knife gap | Set at the knurled knob | 0.05 mm (0.002 in) feeler, smooth along the full cut |
| Lubrication | Linear guide every 100 km (62 miles) of carriage travel, roughly 50 days of single shift use | One pump of green or white lithium grease at the lube ports every 2 months on one shift |
| Blades | VPD3-1CB upper and VPD3-1LB lower, changed as a pair | VPD5-330LK matched knife pair |
If the first cut is not clean
Three things account for most of it, in this order.
- Ragged at one end, clean at the other. The gap is not constant along the cut. Re-run the feeler along the full length rather than adjusting anything at the bad end. That is blade gap and alignment.
- Fiber pull or a fuzzy edge across the whole cut. That is an edge condition, not a setup fault. It belongs in blade life.
- Slow, hesitant or one-sided stroke on the VPD5-330. Check the gauge first, then the flow controls, then lubrication. The full symptom table is in troubleshooting and maintenance.
Not sure which knives your machine takes, or whether the Blade Calibrator came with it? Send us the serial number off the frame and we will confirm it before you order anything.
Setting up a machine you do not own yet?
Both machines ship from the US, and both come with the operation manual, the accessories listed above and a person to call. Tell us the panel size and the score depth you run and we will tell you which one fits, including when the answer is the cheaper one.
Sizes checked? The finder turns your board into an exact part number.